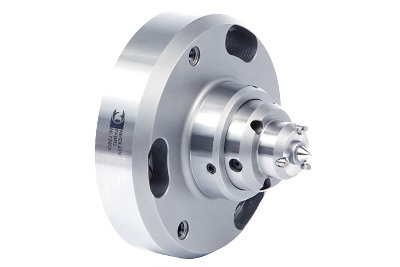
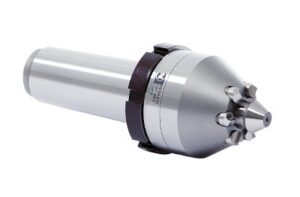
FSB/SB
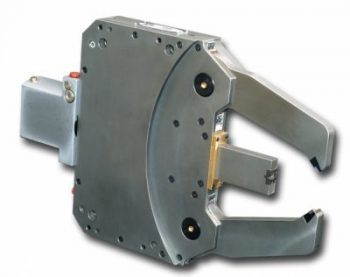
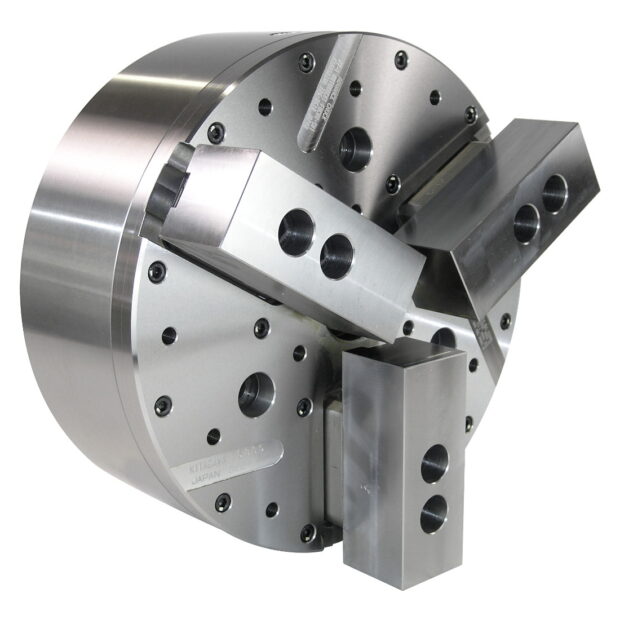
FSB/SB nose cones are driven by the thrust of the rear saddle. The workpiece is clamped centrally by removable pins. This balances the different alignments, which ensures a constant starting point at the end of the workpiece. The "floating" components with a rolling mechanism compensate for unevenness at the end of the workpiece. The maximum actual tolerance is approximately 0.02mm.
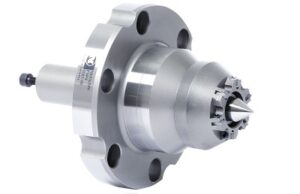
FSP/FSPB
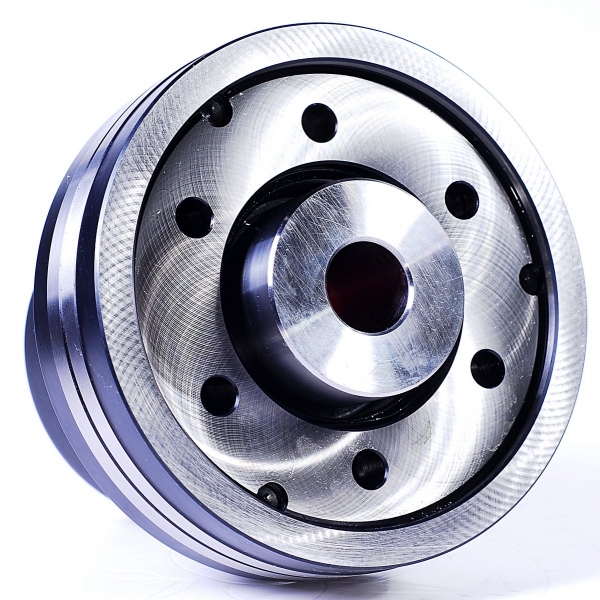
In the FSP/FSPB type end mill cones, the workpieces are gripped by drive discs that are characterized by strength and flexibility of movement diameters. The replaceable inserts, made of carbide, can be changed easily if necessary.
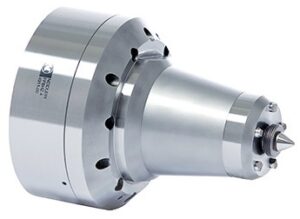
FFB/FFBH
Type FFB / FFBH tapers are driven by the spindle side and the corresponding clamping force on the rear saddle. The parts are secured centrally by a rigid fixed pin, which guarantees high accuracy. The position of the starting point is in the centre of the workpiece.
"Floating" components with a rolling mechanism compensate for unevenness at the end of the workpiece. The FFBH type drive pins are hydraulically compensated, thus achieving the best possible accuracy.
The maximum real deviation is approximately 0.002-0.01mm with FFB type and approx. 0.001-0.005mm with FFBH.
(specifications are process dependent).
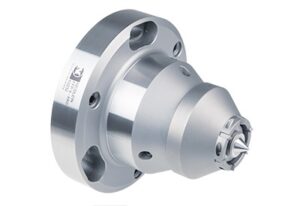
FFP
The FFP type tapers are driven on the spindle side and on the corresponding counter side of the rear saddle. The parts are secured centrally by a rigid fixed pin, ensuring high accuracy. The position of the starting point is in the centre of the workpiece. The workpieces are clamped by drive discs, which are characterized by strength and flexibility of the movement diameters.
The maximum actual deviation is approximately 0.01mm.
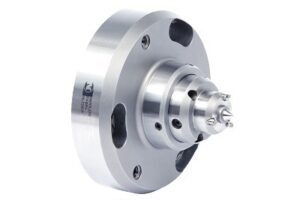
FFBR/FBSR
FFBR/FBSR type tapers are driven by the spindle side and the corresponding clamping force of the rear saddle. The parts are secured centrally by a rigid fixed pin, which ensures high accuracy. The position of the starting point is in the centre of the workpiece.
During pick-up and unloading of workpieces, the drive pins are pulled out. The "floating" components with a rolling mechanism compensate for unevenness at the end of the workpiece.
For maximum accuracy requirements, the tapers can be set with set-screws.
The maximum actual deviation is approximately 0.002-0.006mm.
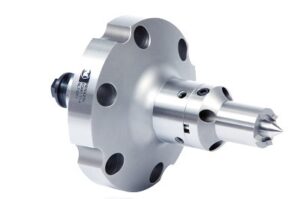
FDNC
FDNC nose cones are driven by the thrust of the rear saddle. The workpiece is clamped centrally by removable pins. This balances the different alignments, which ensures a constant starting point at the end of the workpiece.
The clamping of the drive head allows firm clamping of the workpieces without dead run.
The adjustable, loaded, moving central pin provides the necessary stability and absorption of the transverse shear force.
For maximum accuracy requirements, the tapers can be set with set-screws.
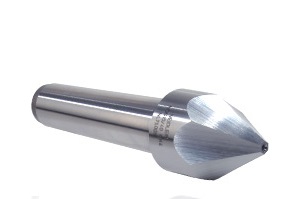
NDG/AND
The NDG/AND tube type cones are driven by the thrust of the rear saddle. The cylindrical workpieces are centered on the face of the cones and are clamped and driven from the contoured end of the cone.